Industrial dust removal system for concrete batch plant
Concrete batch plant produces a large amount of dust during the production process, which mainly comes from the working process of aggregate bins, silos, mixing machines, conveyor belt transfer point and other parts. We provide pulse jet bag dust collector, silo top dust collector, industrial cyclone dust collector, wet dust collection system.
In order to meet the environmental requirements (such as GB 4915 Cement Industry Air Pollutant Emission Standards), it needs to be equipped with effective dust removal equipment. Through the combination of reasonable selection + sealing + dust removal measures, the dust pollution of the mixing plant can be effectively controlled. It is recommended that a professional environmental protection company be commissioned to design the system to ensure that the overall dust removal efficiency is>95%.
AGICO CEMENT offers a wide range of industrial dust collectors for sale with customized service. Our customers can choose cartridge pulse (CP), bag pulse (BP) or reverse air (RA) solution, low-profile round (LPR) or shaker (SK).

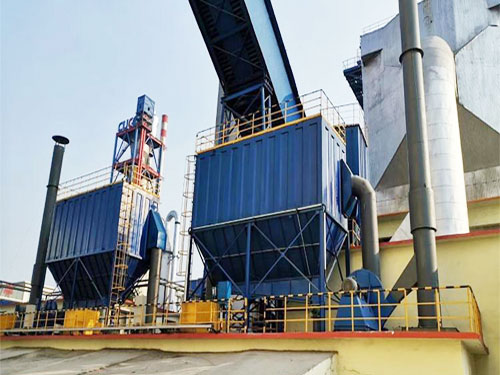
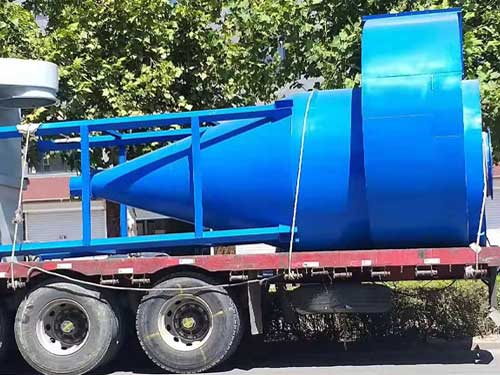

Concrete plant dust collector
| Dust Generation Source | Recommended Equipment | Supplementary Measures |
| Silo Top (Cement/Fly Ash) | Pulse-jet Baghouse Dust Collector (with pressure relief valve) | Install level sensors to prevent overfilling. |
| Mixer Unit | Centralized Pulse Dust Collector + Sealed Enclosure | Adopt negative-pressure design to minimize fugitive dust. |
| Aggregate Feeding Inlet | Cyclone Separator + Spray Dust Suppression System | Add dust curtains to reduce impact-induced dust. |
| Conveyor Transfer Points | Enclosed Hood + Local Exhaust Ventilation (LEV) | Regular cleanup of accumulated dust. |
| Silo Venting Port | Dedicated Silo Top Filter Unit | Inspect filter bags periodically for damage. |
Why choose AGICO CEMENT’s industrial dust collector machine
High energy efficiency filtration
Adopting advanced filter material and technology, realizing high energy efficiency to capture dust particles, and at the same time, reducing filter resistance and prolonging the service life of filter material.
Automatic dust removal
Equipped with automatic dust removal system, the dust removal operation can be carried out automatically according to the accumulation of dust on the filter media, to keep the high energy efficiency operation of the industrial dust removal system.
Energy saving and environmental protection
optimize the structure design, reduce energy consumption, and at the same time realize the recycling of dust or safe disposal, in line with the concept of energy saving and environmental protection.
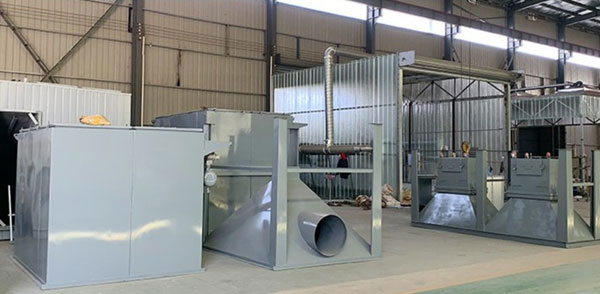
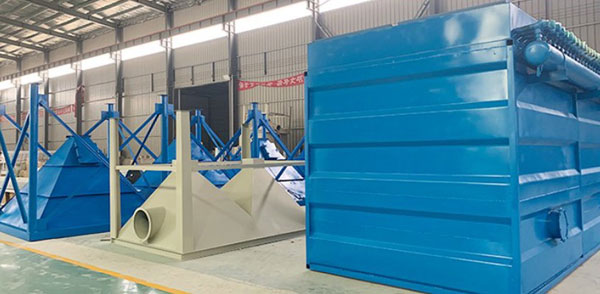
Silo top filter (pulse jet/ bag filter)
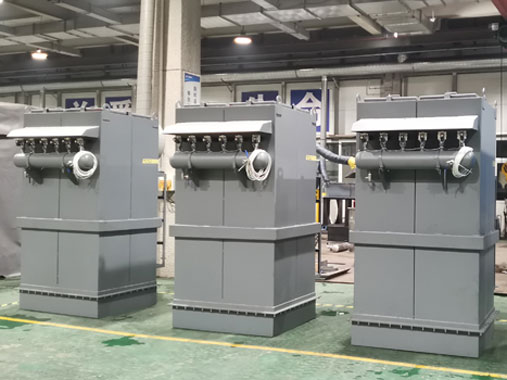
Principle: Installed at the top of the silos, filtering dusty gas when discharging.
Selection: According to the size of the silo and the frequency of feeding to select the air volume (usually 500 ~ 2000m³/h).
Silo top filter (for concrete batch plant dust control) is specially designed for powder filtration of cement, fly ash, mineral powder, etc. By optimizing the pore size and adsorption capacity of the filter element, it ensures high efficiency dust removal.
It can meet the needs of wind conveying for bulk trucks and wind conveying for bagged powder after unpacking, and also can keep the pressure balance in the silo to avoid negative pressure problem and ensure smooth production.
Advantages of AGICO’s silo top filter
High-efficiency dust removal
Adopting high-efficiency filter bag, high dust removal efficiency, up to more than 99%.
Stable operation
Reasonable structural design, reliable dust cleaning system, to ensure the long-term stable operation of the dust collector.
Convenient maintenance
Easy to replace the filter bag and overhaul the dust-cleaning system.
Energy saving and environmental protection
Reduce the dust emission, in line with environmental protection requirements; at the same time, the use of compressed air in the process of dust removal, energy consumption is low.

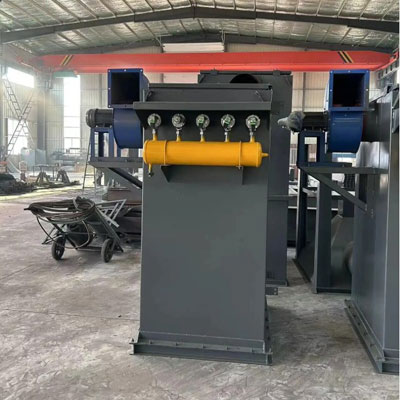
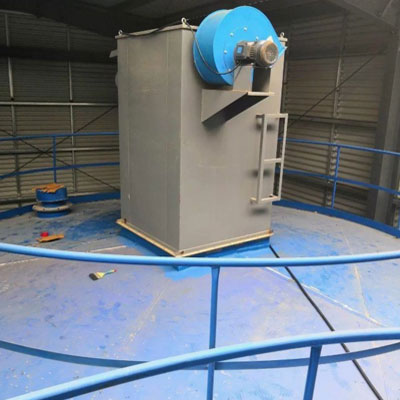
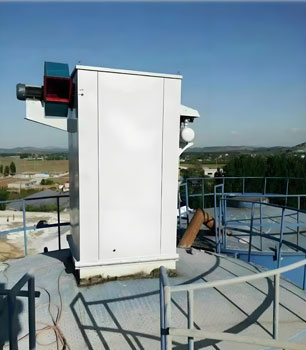
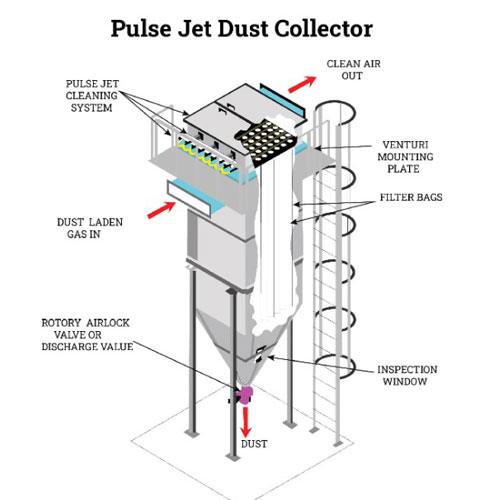
Structure of silo top filter
Air inlet: For introduction of dusty gases.
Pre-processor: e.g. cyclone separator for initial separation of large dust particles.
Filtration chamber: Built-in filter bags for capturing dust.
Purification chamber: Located above the filter bags and collects the purified gas.
Exhaust port: Used to discharge the purified gas.
Pulse cleaning system: including pulse valve, air bag, etc., used for regular cleaning.
Gray hopper: collects the falling dust.
Dust discharging device: such as star unloader, used for discharging dust in the dust hopper regularly.
Working principle of silo top filter
Dusty gas entry: Dusty air enters the dust box from the bottom of the dust collector.
Dust separating:
Coarse particles: directly settle into the dust hopper due to gravity (no filtration required).
Fine particles: intercepted by the surface of the filter bag, forming a dust layer.
Resistance rises: with the accumulation of dust on the surface of the filter bag, the system resistance increases and the airflow decreases.
Automatic cleaning: The pulse valve blows compressed air, instantly shaking down the accumulated dust on the filter bag and restoring the filtration efficiency.
Pulse jet bag filter
Small footprint: adopting high quality raw materials, long service life, compact structure, saving space.
Convenient installation: adopting modularized design, easy to install and replace, exquisite craftsmanship, good sealing after assembly.
Good filtration effect: for fine micron powder, for the average density of 0.5 micron powder
Efficient dust removal: the pulse bag filter has high dust removal efficiency, usually up to 99% or more, which can meet the strict dust emission requirements of the mixing plant.
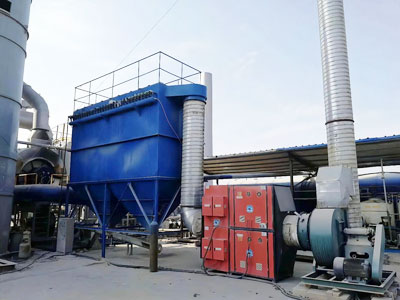
Stable operation: the equipment adopts advanced control system and stable mechanical structure, which can ensure long-term stable operation under adverse working conditions.
Easy maintenance: the bag is easy to replace, and the overall structure of the equipment is compact, which is convenient for daily maintenance and repair.
Strong adaptability: the equipment can be customized according to the specific working conditions and needs of the mixing plant to meet the dust removal requirements of concrete batch with different capacities.
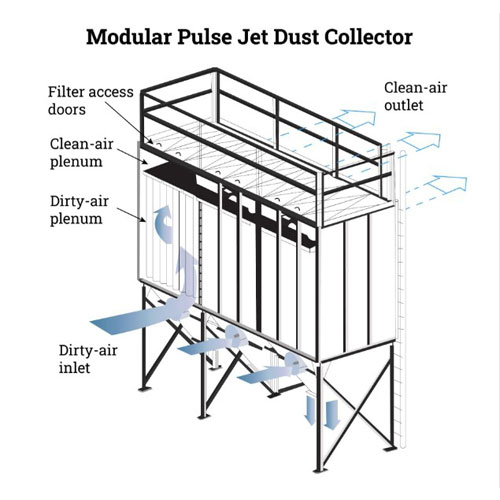
How does the pulse jet bag filter work?
- Dust-containing gas entry: Dust-containing gas enters through the inlet of the dust collector and enters the bag filtration area after pretreatment.
- Dust filtration: When the dust passes through the cloth bag, most of the dust is retained on the outer surface of the cloth bag due to the blocking effect of the cloth bag, forming a dust layer.
- Clean gas discharge: The clean gas after filtered by the cloth bag is discharged into the atmosphere through the air vent.
- Pulse blowing cleaning: With the filtration, the dust layer on the bag gradually thickens, resulting in increased equipment resistance. At this time, the pulse blowing system is activated to spray high-pressure airflow into the cloth bag through the blowing pipe, which makes the cloth bag expand and vibrate instantly, thus shaking the dust layer on the cloth bag down to the dust hopper.
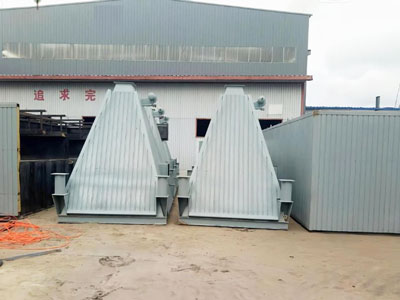
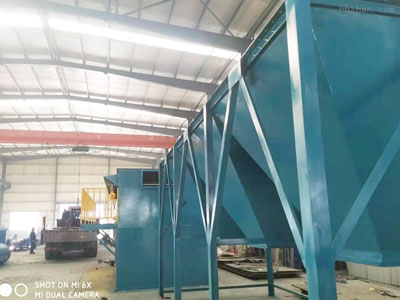
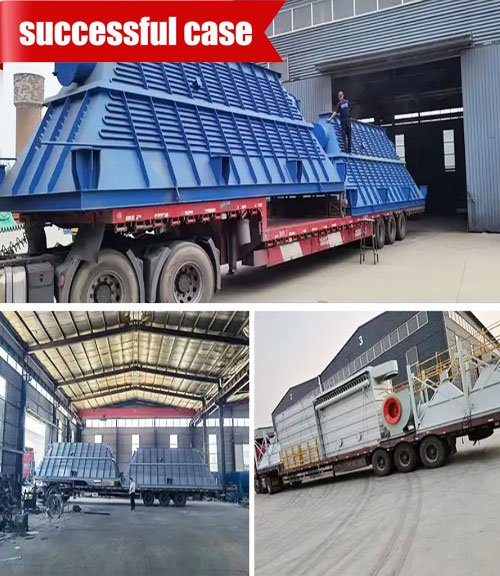
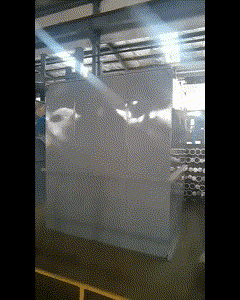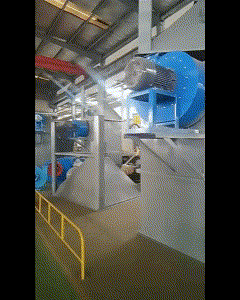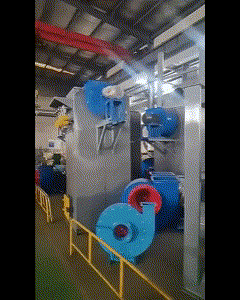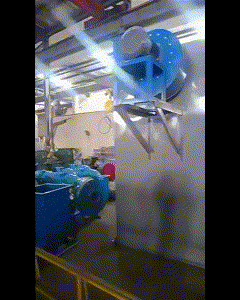
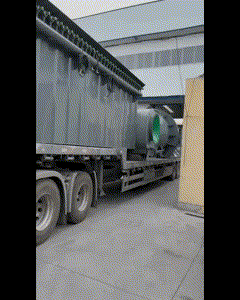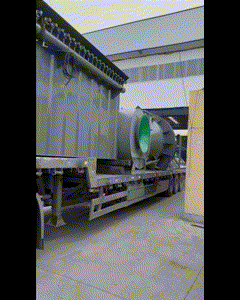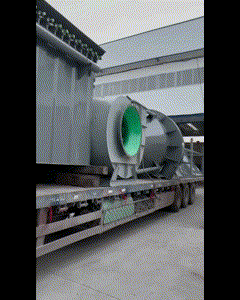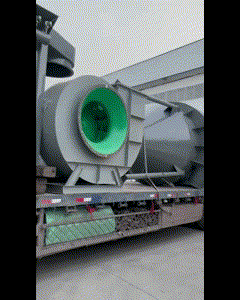
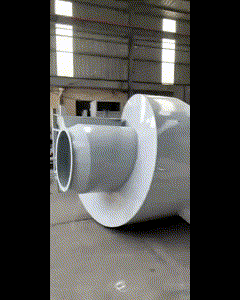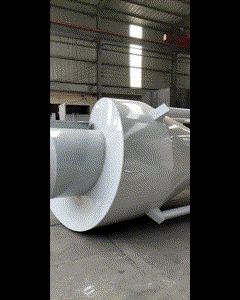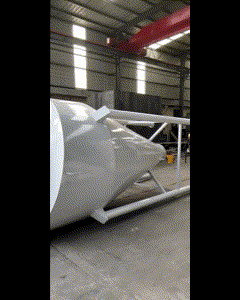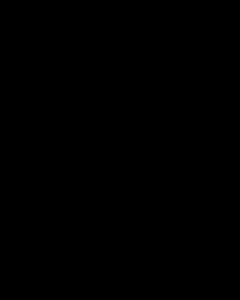
Delivery picture of our industrial dust collector machines

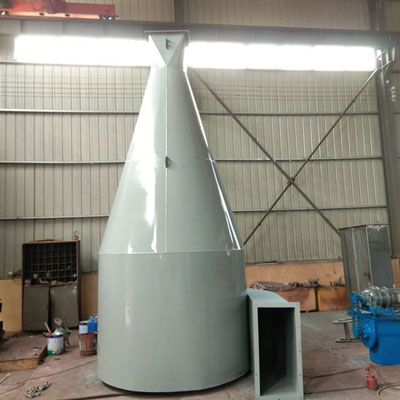
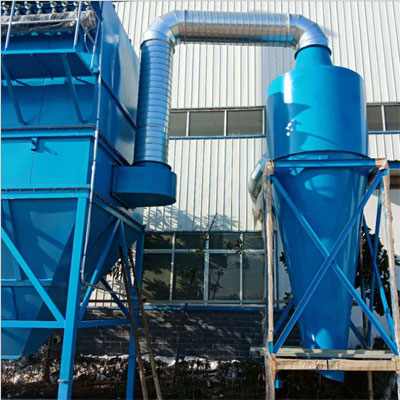
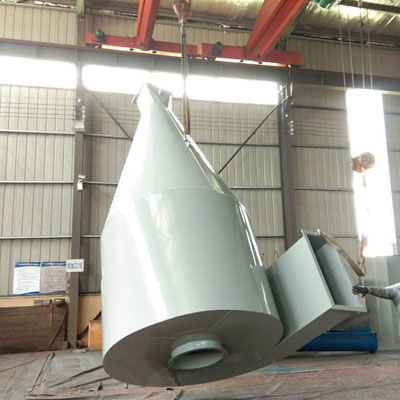
Industrial cyclone dust collector

An industrial cyclone dust collector is a highly efficient dry-type dust removal device that operates on centrifugal force for gas-solid separation.
When dust-laden gas enters the collector, high-speed rotation is generated under the cyclonic effect, causing dust particles to separate from the airflow due to centrifugal force and settle into the hopper at the bottom of the device.
The purified gas is then discharged through the exhaust pipe, achieving the purpose of dust removal.
Advantages of AGICO’s cyclone dust collector
Strict material Selection, attention to detail
Products are manufactured using high-quality raw materials, with no corner-cutting, ensuring reliable quality.
In-house production base, focused manufacturing
With extensive experience and mature craftsmanship, every production step is strictly controlled to provide customers with superior products.
Multiple styles, customizable to needs
A wide variety of product types with broad applicability; non-standard products can be customized according to your requirements.
Ample inventory, on-time delivery
Large stocks of raw materials are maintained, and long-term partnerships with multiple logistics providers ensure timely delivery.
Industrial Cyclone Dust Collector Parameters
AGICO CEMENT’s cyclone dust collector is a highly efficient dust removal device with a collection efficiency of over 95%. The resistance of the collector body does not exceed 900Pa, and it can ensure normal boiler operation when paired with commonly used boiler induced draft fans. The ceramic multi-tube cyclone dust collector offers excellent load adaptability, maintaining a dust removal efficiency of over 94% even at 70% load.
The cyclone tubes inside the dust collector are made of cast iron or ceramic, with a thickness of over 6mm, ensuring wear resistance meets standards. The XD-Ⅱ ceramic multi-tube cyclone dust collector is an ideal solution for industrial boiler flue gas treatment and other dust control applications.
| Model Specification | XD-II -0.5 | XD-II -1 | XD-II -2 | XD-II -4 | XD-II -6 | XD-II -10 | XD-II -20 | XD-II -35 |
| Applicable Boiler (t/h) | 0.5 | 1 | 2 | 4 | 6 | 10 | 20 | 35 |
| Flue Gas Volume (m³/h) | 1500 | 3000 | 6000 | 12000 | 18000 | 30000 | 60000 | 105000 |
| Dust Removal Efficiency (%) | >95 | – | – | – | – | – | – | – |
| System Resistance (Pa) | <900 | – | – | – | – | – | – | – |
| Separator Diameter | 3.05 | – | – | – | – | – | – | – |
| Weight (kg) | 310 | 570 | 960 | 1900 | 2910 | 6100 | 11750 | 20300 |
Advantages of Cyclone Dust Collectors
High Efficiency: Separation efficiency can reach 80% to 95%, effectively capturing dust particles larger than 5 microns.
Low Energy Consumption: Compared to electrostatic precipitators and baghouse filters, cyclone dust collectors do not require additional energy for cleaning systems, resulting in lower operating costs.
Easy Maintenance: Simple structure with fewer components, low failure rate, and convenient upkeep and repairs.
Wide Applicability: Suitable for various high-temperature, high-pressure, and dusty environments, widely used in industries such as chemicals, metallurgy, power generation, building materials, foundries, and grain processing.
Water suppression system for dust
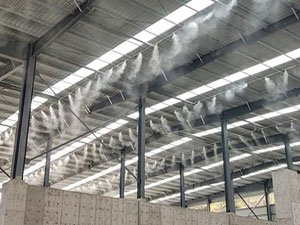
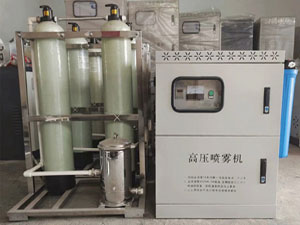
The system sprays fine water droplets that collide with airborne dust particles. The dust particles are captured by the mist, and as the water droplets gain weight, they settle to the ground, preventing dust dispersion. Moreover, the system operates adaptively, equipped with an intelligent control system for smart operation.
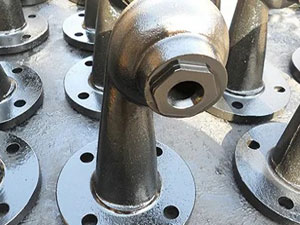
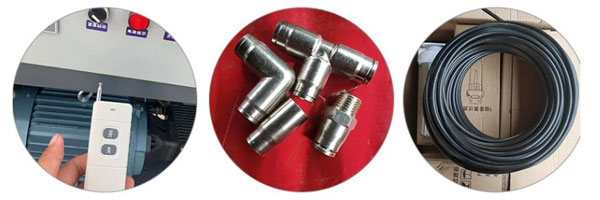
High-Pressure Hose – Long Lifespan
Resistant to low/high temperatures, weathering, and high pressure—durable against impact, ensuring reliable quality.
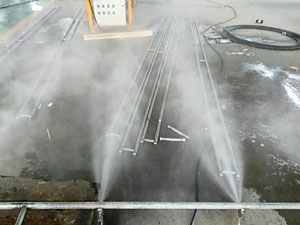
High-Capacity Fog Nozzle
Spray range: 2-3 meters | Mist particle size: 5-10 microns—enhanced atomization for faster dust suppression.
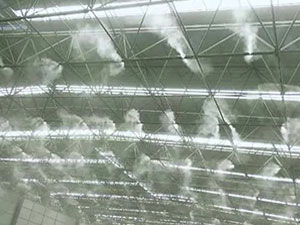
Filtration Unit
Filters impurities in water, effectively preventing sediment from clogging the pump, increasing water pressure.
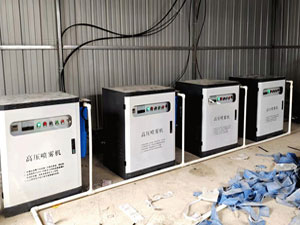
Waterproof Housing
The main unit features a weatherproof enclosure, resistant to outdoor sun and rain.
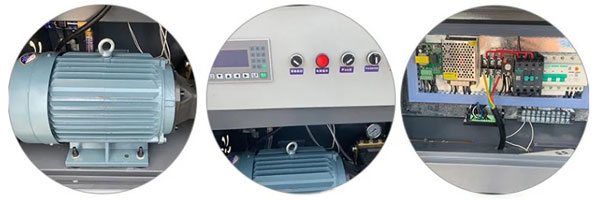
Low-Water Protection
Automatically shuts off when water pressure is insufficient, protecting the pump and motor from damage.
Overload Protection
Prevents power output reduction, ensuring stable and continuous operation.
Smart Control System for Spray Dust Suppression
The system monitors environmental conditions around the silo in real time, including dust concentration, air humidity, temperature, and wind speed. High-precision sensors collect data and transmit it to the central processor of the control system. Based on pre-set programs and algorithms, the processor rapidly analyzes and evaluates the data to optimize dust suppression efficiency.
| Length | 200m | 400m |
| Control Method | Manual, Remote | Manual, Remote |
| Power | 4KW | 7.5KW |
| Nozzle | High-pressure Atomization | High-pressure Atomization |
| Power Supply | 380V | 380V |
| Flow Rate | 20L | 40L |
| Working Pressure | 8-18MPa | 8-18MPa |
| Dimensions | 800*600*1000mm | 800*600*1000mm |
Why choose AGICO as your industrial dust collector manufacturer
Capable
AGICO CEMENT is a high-tech enterprise integrating design, production, manufacturing and installation with 40 years of industry experience
With independent design, independent production workshop, and other strengths of the environmental protection company to meet the market customer special needs; with automatic CNC shearing machine, automatic CNC bending machine, automatic circle round machine and other precision machines.
Design
Design team independent research and development, strong technology, products to promote the development of the industry;
Senior environmental protection engineer tailor-made program 9, more than 15 years of industry engineers to provide customers with worry-free service.
Construction
AGICO CEMENT has a strong on-site installation team, develop technology, installation and construction program, installation schedule before installation; create factory environmental protection solutions for many companies, construction experience is trustworthy
In the late stage of construction, we will provide you with equipment guidance until you learn it.
After-sales
365 days online, quickly respond to any of your questions and give answers in time;
With perfect after-sales service system, the equipment encounters faulty problems, quickly send specialists to the door to solve the problem; with the depth of cooperation with major domestic logistics, to ensure that the goods are quickly delivered to the scene.